Your Cycle Time Is the Cheapest Profit You’ll Ever Find
“We cut three seconds off the cycle and suddenly the same mold, the same machine, the same operator was making 18% more parts a day. Nobody had to buy anything.”
That’s the thing most buyers don’t fully grasp about injection molding: your part cost is set less by the mold price and more by the cycle time. Every second the mold stays closed costs you machine time, labor, energy, and overhead — and shaving seconds off a cycle is often the single highest-return change you can make, because it costs almost nothing to implement.
This guide breaks down where cycle time actually goes, the levers that reduce it (in order of payback), and the mistakes that chase speed at the cost of quality. It’s written for buyers and engineers who want to understand the number that quietly controls their unit cost.
Where Cycle Time Actually Goes
A full injection molding cycle has four phases, and they don’t share the time equally. Understanding the split is the first step to knowing where to cut.
1. Injection (fill) — the shortest phase. Molten plastic is pushed into the cavity. This is typically 10–20% of the cycle, sometimes less. You can’t cut much here, because the plastic has to fill the part.
2. Packing and holding — short but delicate. Pressure is held to pack the part and compensate for shrinkage. Cutting this too aggressively causes sink and short shots.
3. Cooling — the dominant phase. The part must cool until it’s rigid enough to eject without warping. Cooling is almost always 50–70% of the total cycle, which is why it’s the number-one target for cycle-time reduction.
4. Ejection and mold open/close — the overhead. The mold opens, the part ejects, the mold closes again. On a well-run press this is a small slice, but a slow ejector or a sticking part can inflate it.
The practical takeaway: because cooling dominates, the biggest cycle-time wins almost always come from cooling — and everything else is tuning around the edges.
The Cooling Lever: The Biggest Return, the Most Overlooked
Cooling is where the time is, so it’s where the money is. Here are the specific ways to attack it, roughly in order of payback.
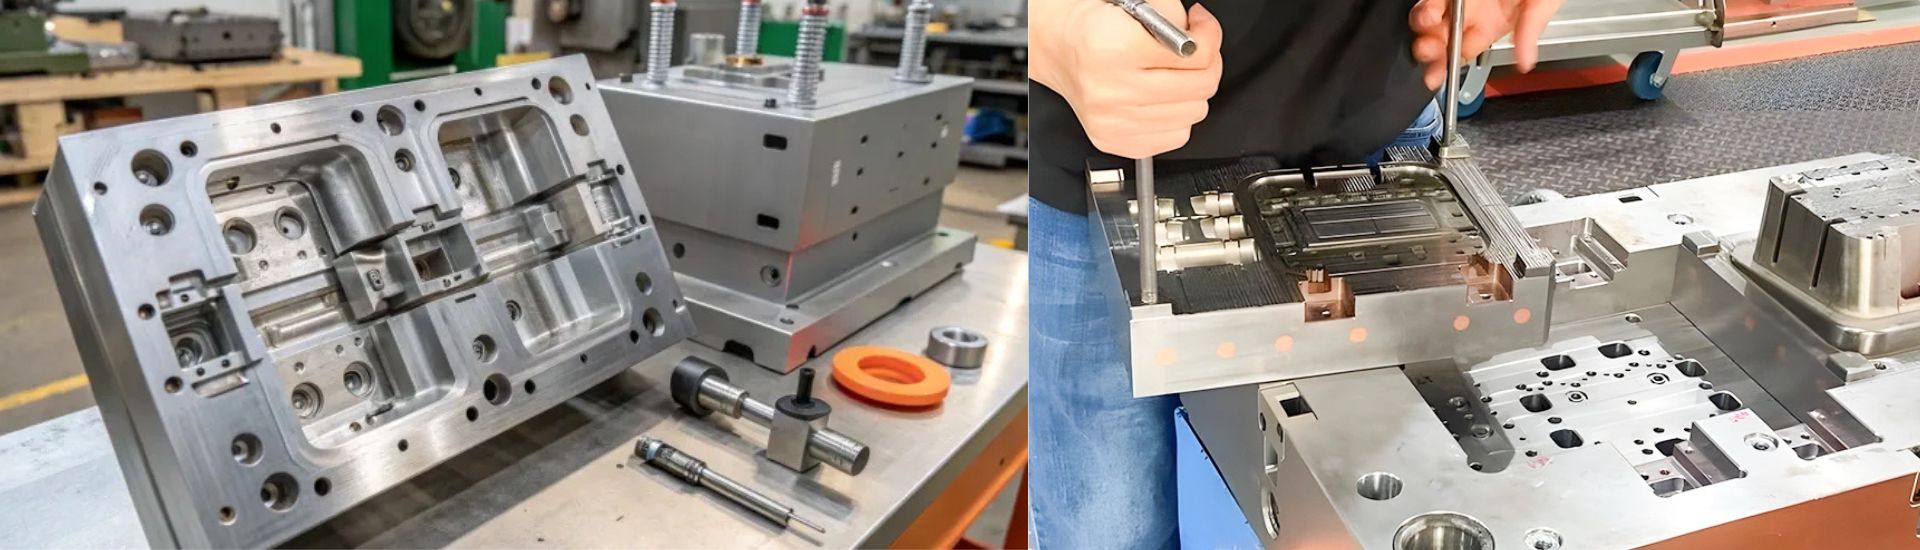
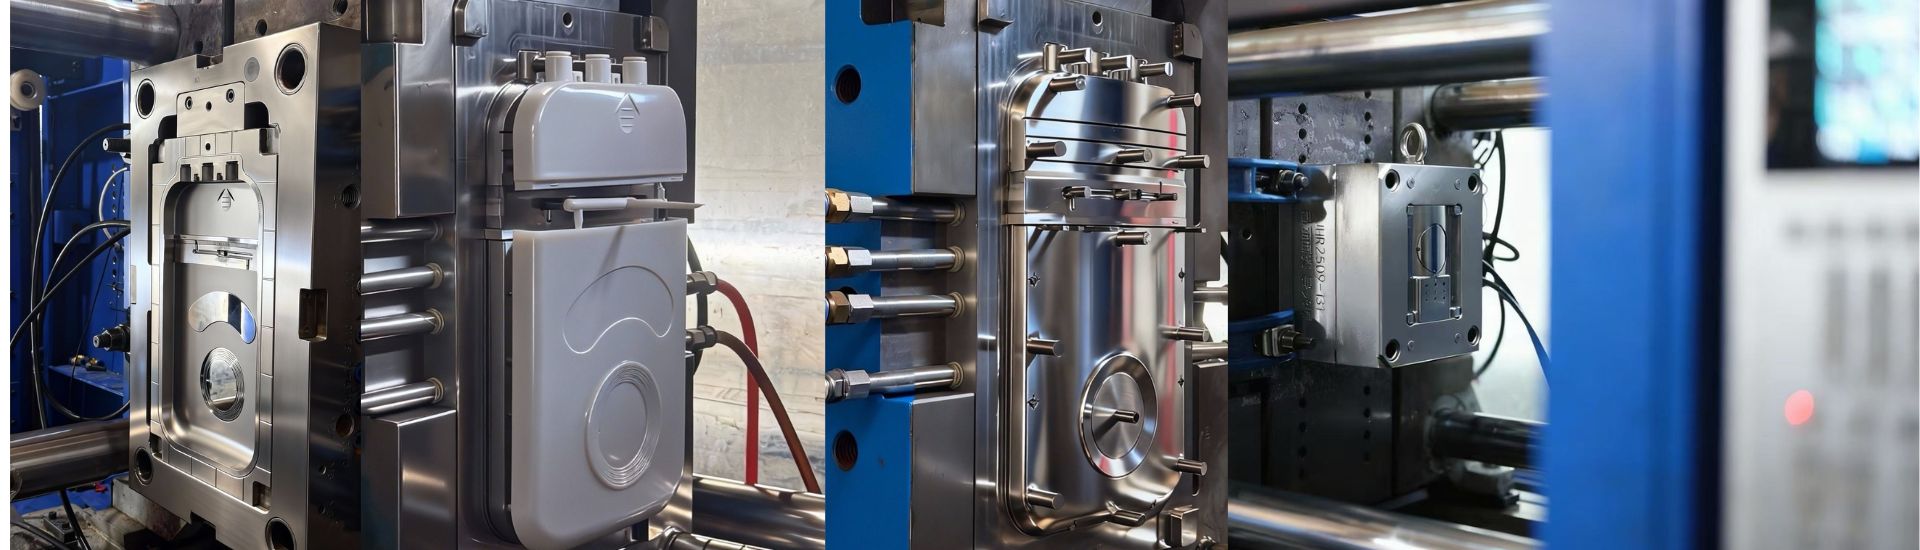
Optimize the cooling-channel design. Water channels placed close to the cavity surface and following its contour pull heat out far faster than a few straight channels drilled through the middle of the steel. A well-designed cooling circuit can cut cooling time by 20–40% on the same part. This is a tooling-design decision, so it has to be made before the mold is cut — our cooling optimization guide covers how to get it right.
Consider conformal cooling for the right part. Conformal channels follow the part’s exact shape, where straight-drilled channels can’t reach. For deep cores, complex geometries, or high-volume parts, conformal cooling can slash cycle time dramatically — but it costs more up front. Whether it pays off depends on your volume and part shape; our conformal cooling explainer walks through the exact trade-off.
Lower the mold temperature where the material allows. A hotter mold gives better surface finish and flow, but a cooler mold shortens the cycle. The trick is to run the mold as cool as the resin and the part’s surface requirements will tolerate — this is a per-material balance, not a fixed number.
Verify the water actually flows. A partially clogged cooling line silently lengthens your cycle while you wonder why the part warped. A simple flow check and regular flushing restores the cooling rate your cycle time was designed around.
Thinner Walls: The Design-Time Lever
The fastest-cooling part is a thin one, because a thin wall reaches ejection temperature in a fraction of the time of a thick section. This is a design decision that has to be made on the drawing board, not the shop floor.
Thinner, uniform walls cool faster and shrink more evenly — two wins that compound into a shorter cycle and fewer rejects. The catch is that thinning a wall too far hurts filling and strength, so there’s a floor for every material. If your part has thick sections that are only there for stiffness, adding ribs instead of wall thickness is the classic fix that cuts both material and cycle time. For the wall-thickness rules that make a part moldable and fast to cool, see our part design guide and the thin-wall molding guide.
Process Tuning: The No-Cost Lever
Once the tool and the part are fixed, the remaining cycle-time wins come from how the press is set up. These cost nothing but a skilled setter’s time.
Don’t over-pack. Holding more pressure than the part needs adds packing time and can over-stress the part. Tune the pack-and-hold pressure to the minimum that produces a good part — you’ll cut the hold time and the internal stress at the same time.
Optimize the screw speed and back pressure. Higher screw recovery can shorten the plasticizing time that overlaps with cooling. If the screw recovery is the bottleneck (which happens on large shots), increasing screw speed or reducing back pressure within the material’s limits recovers cycle time directly.
Match the barrel temperatures to the material. Overheated melt takes longer to cool in the cavity. Running the melt at the low end of the recommended temperature range — while still filling cleanly — shortens the cooling phase.
Tighten the open/close and ejection sequence. Seconds lost to a slow mold open, a hesitant ejector, or a part that hangs up are pure waste. Smooth, fast, well-timed ejection trims the overhead phase with zero risk to quality.
The Levers That Cost Money (and When They’re Worth It)
Some cycle-time reductions require spending, and the question is always whether the payback beats the outlay. Here’s the honest version.
Hot runner systems. A hot runner keeps the runner molten so you’re not cooling and regrinding a cold runner with every shot. For high-volume, multi-cavity tools it can cut cycle time and material waste enough to justify the higher tool cost. For low-volume work it rarely pays — the extra tooling cost outweighs the savings.
Multi-cavity tooling. More cavities means more parts per cycle, which is the most direct way to lower your per-part cost — but it raises the tool price and the required clamping force, and it’s only worth it if your volume justifies the investment. The math on cavity count and tonnage is exactly what our clamping force guide helps you work through.
Higher-grade mold steel. A steel that conducts heat better (or a beryllium-copper insert in a hot spot) pulls heat out of the part faster. It’s a targeted tooling cost that pays off when a single hot spot is dragging out your whole cycle.
Why You Can’t Just Crank the Speed Up
Here’s the warning that matters: cycle time and part quality are in tension, and cutting the cycle blindly produces defects that cost more than the time you saved.
- Cut cooling too short and the part ejects soft — it warps, or sticks, or deforms under the ejector.
- Cut packing too short and you get sink marks and short shots.
- Over-speed the screw and you shear-degrade the material, especially glass-filled and heat-sensitive resins.
- Push fill too fast and you get jetting, flash, or a burned part from trapped gas.
The right approach is to reduce cycle time methodically — one lever at a time, verifying part quality at each step — not to set the press to “fast” and hope. If a reduction starts producing defects, back off. Our defect guide maps each symptom back to the process variable that caused it, so you know exactly what you over-tightened.
The One Rule That Governs Everything
If there’s a single principle behind every cycle-time reduction, it’s this: remove heat from the part as fast and as evenly as possible, and don’t spend time doing anything that doesn’t move heat or move the part.
Cooling dominates the cycle, so the fastest path to a cheaper part is a mold that cools efficiently, a part that’s no thicker than it needs to be, and a press that’s tuned to pack just enough and eject smoothly. Everything else — hot runners, multi-cavity, premium steel — is an investment decision that follows from your volume.
How to Ask Your Molder the Right Question
When you’re sourcing a mold, don’t just ask for the price — ask about the cycle time, because it’s the number that determines your long-run cost. The three questions that separate a molder who thinks about your unit cost from one who just cuts steel:
1. “What’s your predicted cycle time for this part, and how did you arrive at it?” A molder who runs mold-flow analysis can predict the cycle time before cutting steel — and can tell you what they’d change to shorten it. A molder who can’t answer this is guessing.
2. “What did you do in the tool design to optimize cooling?” Listen for the specifics: channel placement, conformal cooling where it matters, steel selection in hot spots. Vague answers mean a tool that will run slower than it should for its entire life.
3. “Can you show me the cycle-time breakdown and what levers are left on the table?” A serious molder treats cycle time as a number they own and can defend, not a number they hope for.
Get a Mold That’s Built for a Fast Cycle from Day One
Cycle time isn’t something you discover after the mold arrives — it’s something that should be engineered into the tool from the first design review. A mold with optimized cooling, sensible wall thickness, and a clean ejection setup will run faster and cheaper for its entire life, and that difference shows up in every single part you ever make.
That’s the conversation we have before we cut steel: we run the mold-flow analysis, design the cooling for your specific part and volume, and tell you the predicted cycle time before you commit. Send us your STEP file and tell us what the part does — we’ll give you a DFM review and a quote within 12 hours, with cycle time on the table from the start.