What Is Two-Shot Injection Molding?
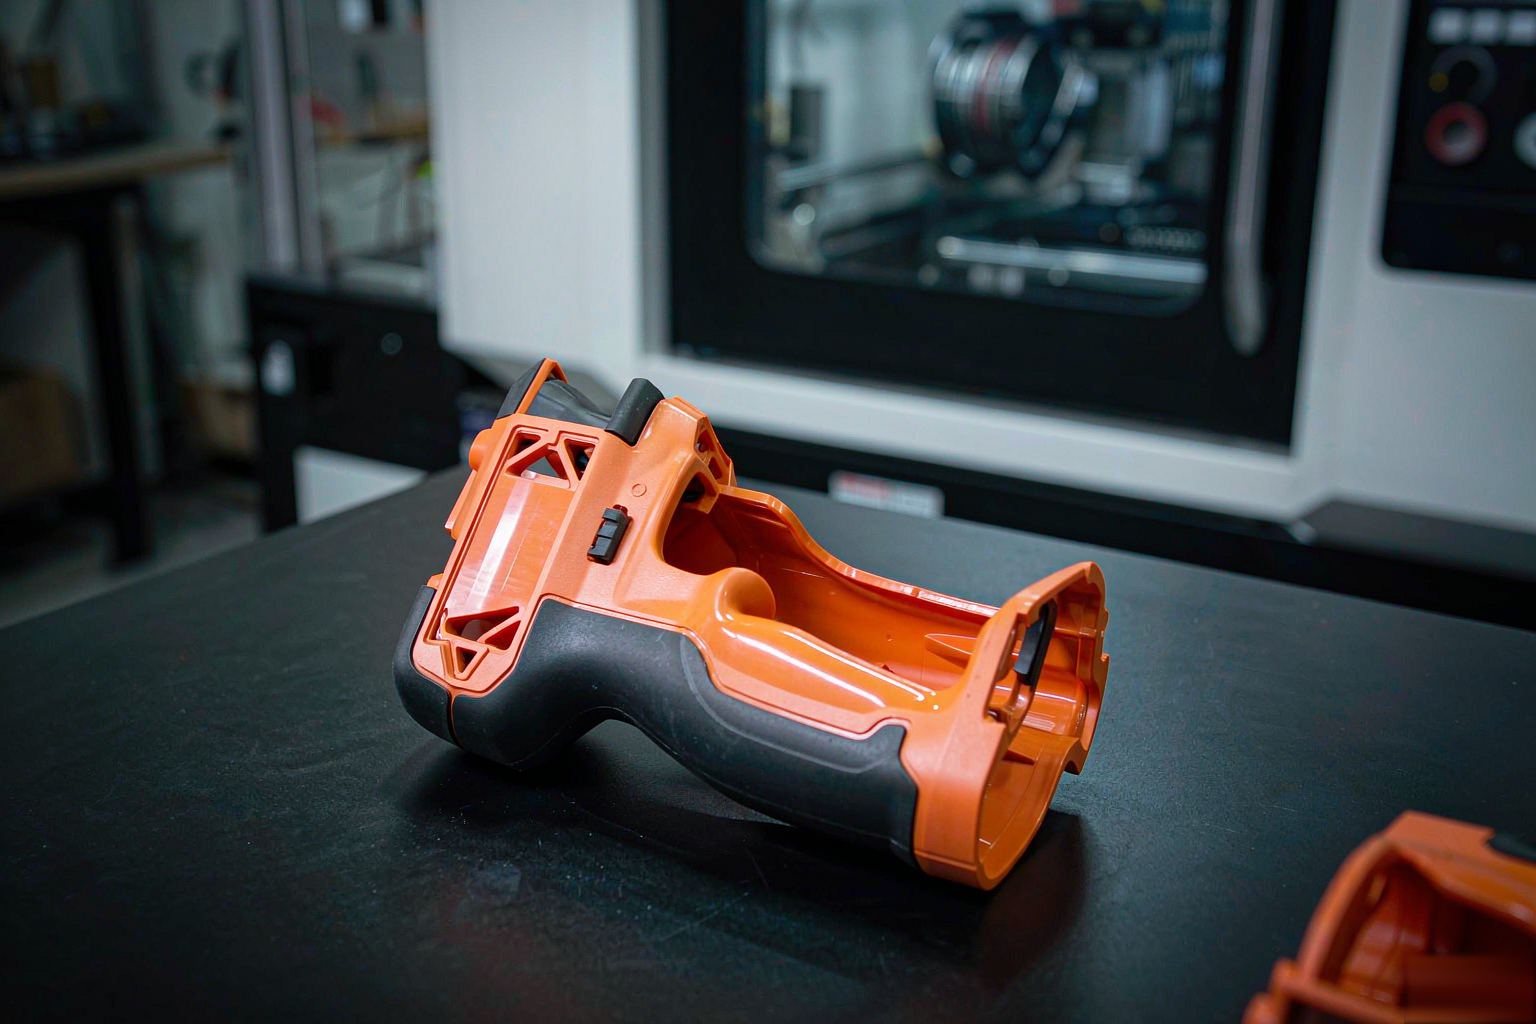
Two-shot injection molding (also called two-color, 2K or multi-shot molding) combines two different plastic materials or colors into a single part within one molding cycle. The first material is injected into the mold cavity; the mold then rotates or slides so the second material is injected and bonds to the first. The result is a single integrated component with two materials or colors — produced without secondary assembly steps, adhesives or manual handling.
The classic example is the power tool housing: a rigid body for structure, with a soft, grippy, chemical-resistant overmold exactly where the hand lands. Two-shot molding scales that idea across industries — any place where a part needs two behaviors at once.
Benefits of Two-Shot Molding
- Eliminates secondary assembly — soft grips, seals and buttons are molded directly onto the part, reducing labor, handling and glue-related quality risks
- Improved part strength and durability — materials are chemically or mechanically bonded in the mold for a joint that outlasts adhesives
- Design flexibility — combine hard and soft materials, translucent and opaque windows, or two colors in one part
- Lower total cost at volume — fewer parts, no assembly station and tighter tolerances than over-molding in separate operations
- Better sealing performance — continuous soft layer molded in position seals more reliably than a glued gasket
Two-Shot Molding Applications
- Consumer electronics — buttons, keypads, seals and soft-touch housings
- Medical devices — ergonomic grips and color-coded components
- Automotive — knobs, switches, interior trim and seals
- Household and appliance parts — handles, grips and gaskets
- Power tools and industrial equipment — overmolded grips and protective layers
Common Material Combinations
Two-shot success starts with material compatibility — the two resins must bond, and their shrinkage must be compatible. Frequently run combinations:
| Rigid Substrate | Soft / Second Shot | Typical Application |
|---|---|---|
| PP | TPE / TPV | Appliance grips, seals, tool handles |
| ABS | TPU / TPE | Electronics housings, soft-touch keys |
| PC | TPE | Device grips, seals on rigid windows |
| PC/ABS | TPU | Power tool bodies, industrial grips |
| PA (nylon) | TPE | Under-hood grips, vibration parts |
| Same resin, two colors | — | Color-coded buttons, indicators, keypads |
Bonding, shrinkage mismatch and thermal compatibility are reviewed during DFM — before the mold is quoted — so the second shot bonds every time, not only at the trial. If your part needs a rigid layer with inserts instead, see our insert molding services; for overmolding on complete substrates, see overmolding services.
Two-Shot Mold Manufacturing at D-top Mould
Two-shot molds are precision machines in their own right: the first and second shots must align within hundredths of a millimeter across millions of cycles. We design and build rotating-platen and sliding-core two-shot molds in-house, with mold flow analysis on both shots, precise alignment of the first and second cavity positions, and trial validation of bonding quality before mold shipment. We support both new two-shot tooling and the optimization of existing multi-shot molds.
Two-Shot vs Secondary Overmolding vs Assembly
| Approach | Best For | Watch-outs |
|---|---|---|
| Two-shot molding | High volumes, tight tolerances, bond-critical parts | Higher mold investment |
| Secondary overmolding | Medium volumes, simpler geometry | Handling cost, bond consistency |
| Adhesive assembly | Low volumes, dissimilar materials | Labor, glue aging, alignment variance |
Not sure which route fits your volume? Our free DFM review compares the real numbers — mold investment, cycle cost and quality risk — so the decision is economics, not guesswork. For a deeper cost discussion, see our article on when two-shot molding is worth the extra cost.
Why Choose D-top Mould for Two-Shot Molding
- In-house two-shot tooling — design, machining and trials under one roof, with stable T1 results
- 12-hour quotation — send both materials and the 3D model, receive an engineered quote within 12 hours
- Fast mold modifications — bonding or alignment adjustments handled quickly by our own tool shop
- Flexible scheduling — prototype and production volumes supported without long queues
- Responsive after-sales support — mold maintenance and process support across the program life
Frequently Asked Questions
Q: What is two-shot injection molding?
A: Two-shot (2K) injection molding molds two different plastics or colors into a single part in one machine cycle. The first shot forms a rigid substrate; the mold rotates or the part transfers to a second cavity where the second material is injected and bonds to the first — with no adhesive and no assembly step.
Q: How much more expensive is a two-shot mold than a single-shot mold?
A: Typically 30–60% more, because a two-shot mold is effectively two molds in one body — two cavity sets, rotation or core-pull mechanics and more tuning. A single-cavity two-shot mold commonly starts around USD 10,000 and rises with cavitation and complexity. It can still pay for itself by deleting assembly labor at volume.
Q: Which materials can be combined in two-shot molding?
A: Compatible pairs bond best: TPE or TPU onto PP, ABS or PC for soft grips; TPV onto PP for molded seals; and rigid pairs such as PC/ABS or POM/PA for two-color parts. Incompatible pairs need mechanical interlock features.
Q: When should I choose two-shot molding instead of overmolding?
A: Choose two-shot at high volume (roughly 50,000+ parts per year) when you need a permanent bond and want to delete assembly. Choose conventional overmolding at lower volumes or when the second material can be added off-line more cheaply.
Q: What is the minimum volume for two-shot injection molding to be cost-effective?
A: Roughly 50,000 parts per year is the common break-even, depending on the assembly cost you eliminate. Below about 10,000 parts, secondary overmolding or assembly usually costs less.
Get a Two-Shot Molding Quote in 12 Hours
Send your 2D or 3D drawings, the two materials (or colors) you plan to use, expected annual volume, part appearance and tolerance requirements. Our engineering team reviews bonding compatibility and alignment strategy, then responds with a free DFM review and a detailed quotation within 12 hours — so you know the mold investment, the cycle economics and the risks before committing to steel.