Why Your “Solid” Plastic Part Might Be Working Against You
“We asked three tooling shops whether our 40 mm handle needed gas-assist, and we got three different answers — one said it’s mandatory, one said it’s a gimmick, and one said to just add more ribs and wall it up.”
That’s a real conversation we hear from product engineers more than you’d think, and it usually comes from the same place: the part is thick, the customer wants it light and rigid, and nobody has explained exactly what gas-assisted injection molding (GAIM) actually does to the plastic — and what it does to your tooling budget.
This guide explains the mechanism in plain terms, the four situations where gas-assist genuinely pays off, the three situations where we would honestly tell you to skip it, and the design rules that keep a gas-assist mold from becoming a money pit. It’s written for buyers and engineers who need to make a call, not for people who already own a molding plant.
What Gas-Assisted Injection Molding Actually Is
Standard injection molding fills a cavity completely with molten plastic under high pressure, then packs more plastic in to compensate for shrinkage as it cools. Every gram of that plastic has to be injected, packed, and cooled — and cooling is almost always the slowest step in the cycle.
Gas-assisted injection molding changes the last step. After the cavity is partially filled with resin (typically 60–95% by volume), an inert gas — almost always nitrogen — is injected under controlled pressure. The gas pushes the still-molten plastic outward against the cavity walls and, critically, hollows out the interior into a series of hollow channels. The result is a part with a smooth, thick-walled skin and a hollow core, all formed without a second material or a secondary operation.
Think of it as the plastic equivalent of a bicycle frame tube instead of a solid rod: most of the mechanical stiffness of a beam comes from its outer surface, not its center, so removing the center costs you little stiffness while saving a large share of the weight and cooling time.
How the Gas Flows: The Two Main Methods
There are two distinct ways to introduce the gas, and they produce different internal geometries, so it’s worth knowing which one a supplier proposes before you sign off.
Short-shot / full-shot gas-assist. The cavity is deliberately under-filled, then gas is injected through the nozzle or a gas pin to push the melt to the cavity walls and hollow the center. This is the workhorse method for thick-walled parts and handles.
Gas-through-nozzle vs. gas-through-pin. Gas can enter through the machine nozzle (cheaper, but gas flow follows the melt flow path and is harder to control) or through dedicated gas pins placed in the tool (more tooling cost, but the gas channels can be positioned precisely where you want the hollow sections). For load-bearing parts where the gas channel must not wander into a thin wall, gas pins are usually the right call.
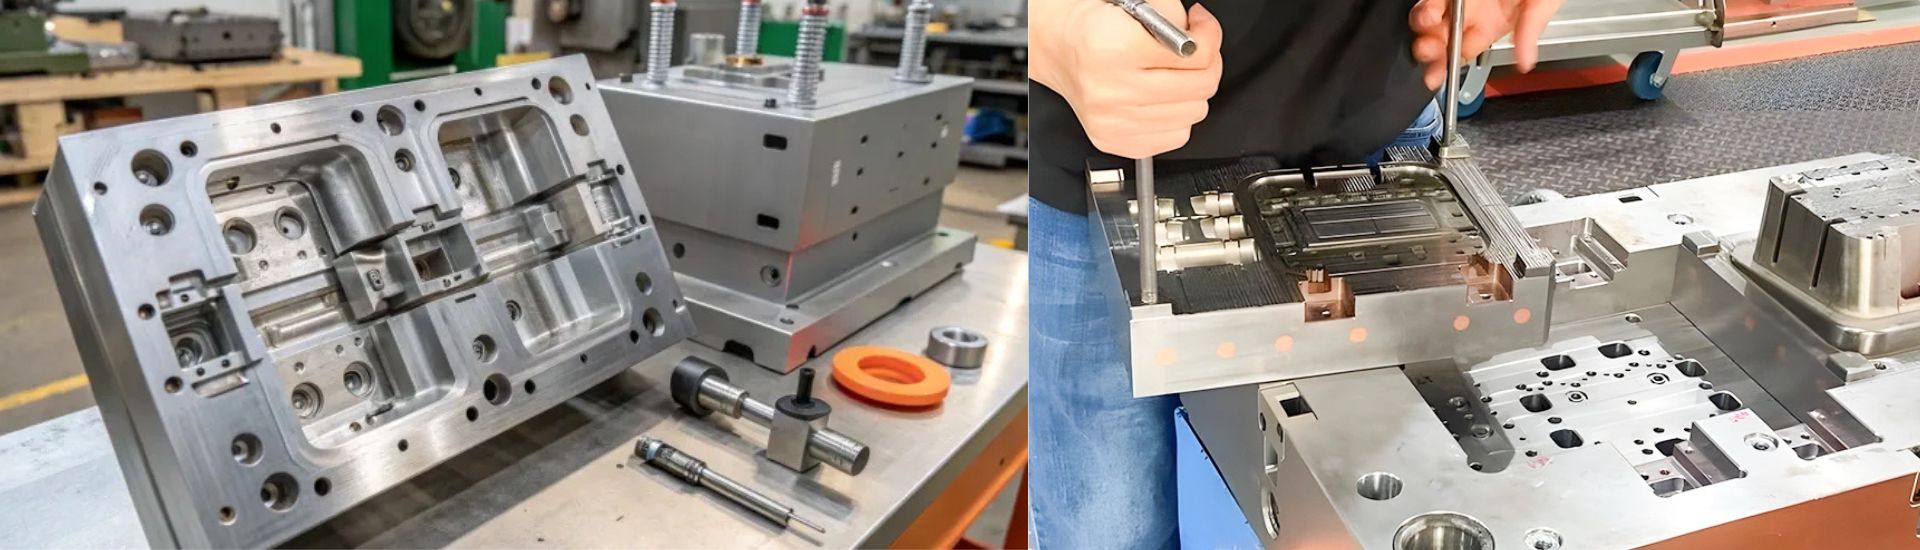
The gas channel itself is the key design feature: as the gas cores out the center, it follows the path of least resistance, which the mold designer directs by building slightly thicker “gas channel” ribs into the part. Get those channels wrong and you get a hollow that wanders, a wall that pinches closed, or a finger-thin blowout.
When Gas-Assist Genuinely Pays Off
Here’s the honest version. Gas-assist is not a universal upgrade — it’s a solution to a specific set of problems, and if your part doesn’t have those problems, you’re paying extra tooling cost for nothing.
1. Thick walls with sink marks. Any wall over roughly 4 mm is at risk of sink marks and long cooling times. Gas-assist hollows the wall from the inside, which eliminates sink and slashes cooling time. This is the single most common reason people choose GAIM.
2. Long, thick structural sections. Handles, frames, brackets, automotive grab handles, furniture arms, appliance grips — parts that need beam-like stiffness but would otherwise be heavy and slow to cool. Hollowing them keeps stiffness while cutting weight and cycle time.
3. Weight reduction that matters. In automotive and large-appliance work, shaving 20–40% of the resin weight from a structural part is real money at production volumes, and it also lowers the clamping force required to hold the tool shut.
4. Combining wall thickness changes in one part. When a part has both thick bosses and thin ribs, gas-assist can help balance the filling so the thick areas don’t drag the cycle out while the thin areas freeze off.
In all of these cases the payoff shows up as faster cycle time, lower part weight, less sink and warpage, and sometimes a smaller press — which is why, for the right part, the extra tooling cost is recovered quickly. We walk through the exact trade-off in the section below.
When We’d Tell You to Skip It
Being straight with you: there are at least three situations where we advise a customer against gas-assist, even though it would add to our invoice. These are the “failure conditions” that a good DFM review should flag before any steel is cut.
Thin, uniform walls. If your part is mostly 1–2.5 mm walls with no thick sections, there’s nothing to hollow out. Gas-assist would just blow through the thin wall or leave you with a part no lighter than a standard molded one. Standard molding wins on both cost and simplicity.
Cosmetic Class-A surfaces. Gas channels can leave a faint internal witness or surface swirl on high-gloss, grained, or painted surfaces. If the part is a visible exterior panel, gas-assist adds risk to the finish, and the cost of a rejected batch is worse than the resin you’d save.
Tight dimensional control on thin features. Because the gas pressure (typically 5–15 MPa) is much lower than full packing pressure, gas-assist parts can’t always hold the same tight tolerances on fine features as fully packed solid parts. If you need ±0.05 mm on thin ribs, gas-assist is probably not your friend.
For more on the kinds of design flaws that make any mold risky, our DFM checklist walks through seven rules that save money before steel is cut.
The Real Trade-Off: Tooling Cost vs. Cycle Time
Gas-assist adds cost in three places: the gas injection unit (either a machine retrofit or a portable nitrogen generator/controller), the gas pins and channels machined into the tool, and the extra engineering to simulate and position the gas channels. This is why GAIM tools typically run more than a comparable standard tool of the same size.
What you get back, on the right part, is usually a meaningful cut in cycle time — because the hollow core cools faster than a solid section of the same nominal wall — plus lower resin weight and less clamp force. The math works when the cycle-time and material savings over your expected volume exceed the added tooling and equipment cost.
The honest way to find out whether it works for your part is a mold-flow analysis with gas channel simulation, not a supplier’s sales pitch. Ask your molder to show you the predicted gas channel path, the predicted wall thickness after gas, and the predicted cycle-time delta before you commit to the extra tooling.
Materials That Work (and a Few to Watch)
Gas-assist works with most thermoplastics, but some are friendlier than others. Resins with higher melt strength hold the gas channel shape better and resist gas blow-through in thin sections.
Well-suited: PP, PE (including HDPE), ABS, PC/ABS, PA (nylon), PBT, POM, and most filled grades like PP with glass fiber. These hold a stable gas channel and are the materials you’ll see in 90% of GAIM applications.
Use with care: very low-viscosity resins (some high-flow grades) can let gas blow through or leave a rough internal surface; highly crystalline materials with high shrinkage need careful channel sizing so the hollow doesn’t collapse as the part shrinks. Material shrinkage is exactly why channel sizing matters — see our shrinkage rate chart by material to understand what each resin does as it cools.
Glass-fiber-filled grades deserve a note: they’re excellent for stiff, lightweight structural parts, but the fibers slightly roughen the gas-channel interior, which is fine structurally but worth knowing if the part is ever to be inspected internally.
Design Rules That Keep a Gas-Assist Mold from Becoming a Money Pit
If you do go the gas-assist route, these rules are the difference between a tool that runs for 300,000 shots and one that fights you from T1:
- Design the gas channel deliberately. The hollow follows a thicker “channel” rib you build into the part. Don’t let the gas decide for itself — it will take the shortest, weakest path and ruin the part. Typical channel cross-section runs 2–3× the adjacent wall thickness.
- Keep the channel continuous and let it vent. The gas needs somewhere to go and a way to relieve pressure at the end of the shot. A dead-ended channel traps gas and creates a weak blowout point.
- Watch the gas-entry location. Gas should enter where it can push the melt outward evenly, not where it will jet across a thin feature or race a weld line. Gas entry near the gate usually helps; entry far downstream can cause hesitation.
- Mind wall-thickness transitions. Abrupt steps in wall thickness create spots where the gas channel pinches off or balloons. Keep transitions gradual.
- Account for draft and ejection. Hollow sections are no easier to eject than solid ones, so the same draft angle rules still apply — and a gas-assist part that’s too thin on the ejector side can stick.
The One Number Most Articles Leave Out
Here’s a hard, checkable figure we don’t see competitors publish: the gas pressure and hold time are what actually set your surface quality and cycle time, and they’re far lower than people assume. Typical gas injection pressure runs roughly 5–15 MPa (about 50–150 bar), injected for only a fraction of a second, then held at a lower pressure while the part cools. By contrast, full melt packing pressure in a standard mold is often 40–100+ MPa. That 5–15 MPa gas pressure is what hollows the core — and it’s also why gas-assist can’t pack fine thin features as tightly as solid molding, which loops back to the tolerance warning above.
If you want a reference point for the machine side of this, the clamping force still has to resist the plastic pressure trying to open the tool — our clamping force (tonnage) guide explains how to size the press for your projected area.
Gas-Assist vs. the Alternatives: A Quick Comparison
| Approach | Best for | Weight / cycle | Relative tool cost |
|---|---|---|---|
| Standard molding (solid) | Thin, uniform walls; tight tolerances | Heavier, slower on thick sections | Lowest |
| Gas-assisted (GAIM) | Thick, long structural sections; sink-prone walls | Lighter, faster cycle | Higher |
| Water/foam assist (WIT / structural foam) | Very large, low-stress panels | Lighter but coarser surface | Higher |
| Add ribs / wall up instead | Simple parts that can tolerate extra material | Heavier, no tooling change | Lowest |
The comparison that matters most is usually the last row: before you spend money on gas-assist, ask whether the part could just be redesigned with ribs and a slightly thicker wall. If the answer is yes, skip gas-assist. If the part genuinely has a thick structural section you can’t wall up, gas-assist is the right conversation to have.
How to Spec Gas-Assist in Your RFQ (Without Getting Three Different Answers)
When you send a gas-assist part out for quote, the single best thing you can do is give the supplier a clear description of the part’s function and the thick sections, and ask for the simulation, not just the price. Send these with your RFQ:
- A STEP or IGES 3D file of the part (not just a PDF drawing)
- The resin and, if possible, the grade and MFI
- The expected annual volume (this decides whether the tooling premium is worth it)
- Which surfaces are cosmetic and which are functional
- Any weight target, if you have one
Then ask the supplier for three things: a predicted gas-channel path from mold-flow analysis, the predicted wall thickness after gas, and the predicted cycle time versus a solid part of the same shape. A shop that can produce those three answers is one that actually understands gas-assist — a shop that can’t is guessing.
Get a DFM Review Before You Cut Steel
Gas-assisted injection molding is one of those technologies where the decision matters more than the execution. Done on the wrong part, it’s wasted money; done on the right part, it can cut weight, speed up your cycle, and eliminate sink marks on a part that would otherwise be a headache.
That’s exactly what a DFM review is for. Send us your STEP file and tell us what the part does — we’ll tell you honestly whether gas-assist is worth it for your part, show you the predicted gas channel and cycle-time delta, and quote the tool. No pressure, no “gas-assist solves everything” pitch — just a straight answer with numbers behind it. Contact D-TOP MOLD and you’ll have a DFM review and a 12-hour quote back.